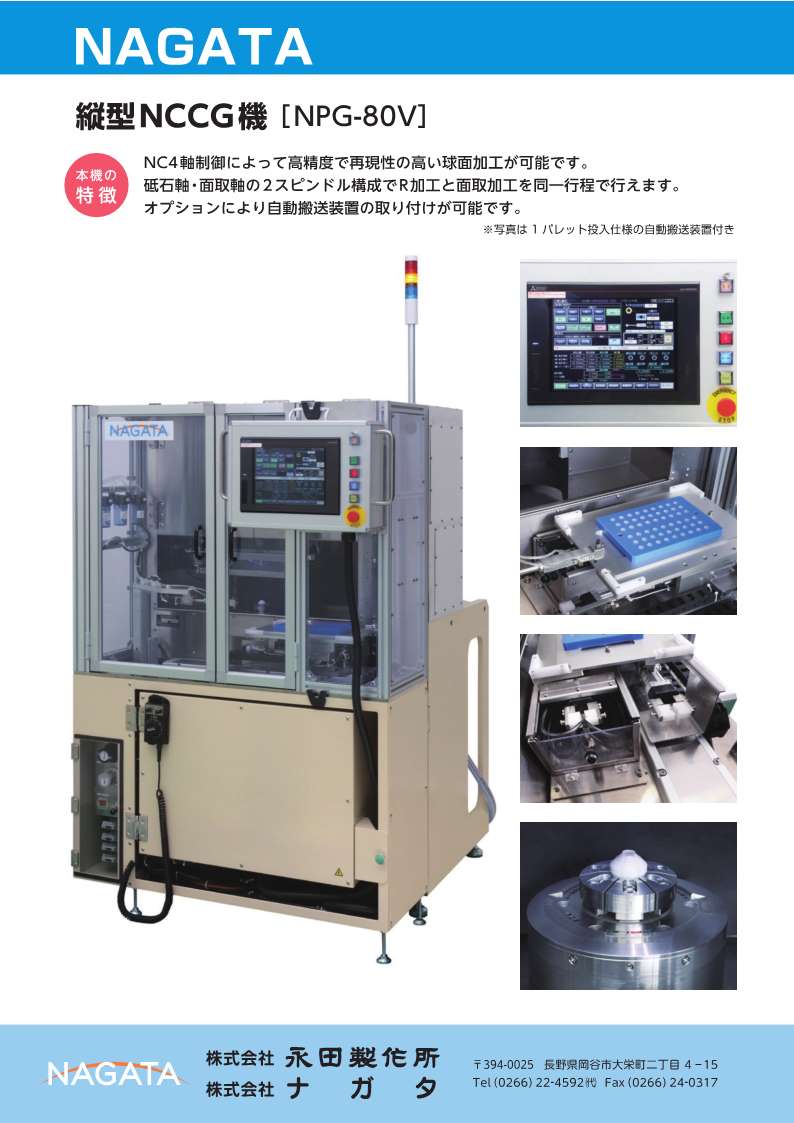
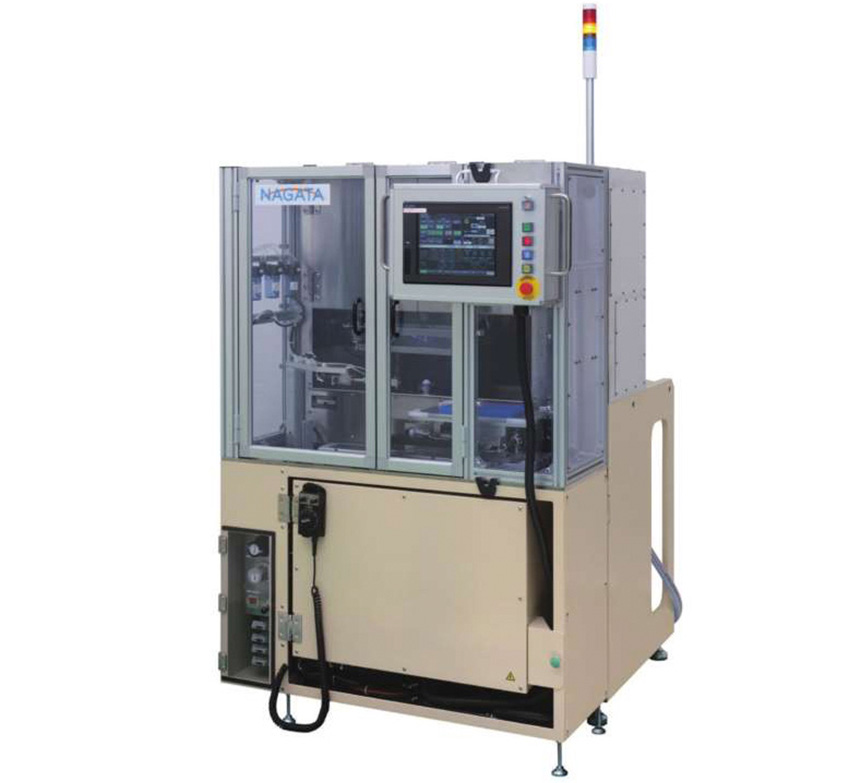
NC control allows automatic setting of machining conditions by inputting information on the target workpiece and grinding wheel. In addition, automatic compensation functions (convexity correction and Δh correction) allow processing conditions to be corrected simply by inputting the measured values of test-cut workpieces.
Grinding wheel feed function is provided according to the number of times the grinding wheel is processed to compensate for wheel wear.
The use of an optional automatic transporter enables automatic feeding of workpieces and continuous processing of workpieces.
A chamfering axis can be attached as an option.
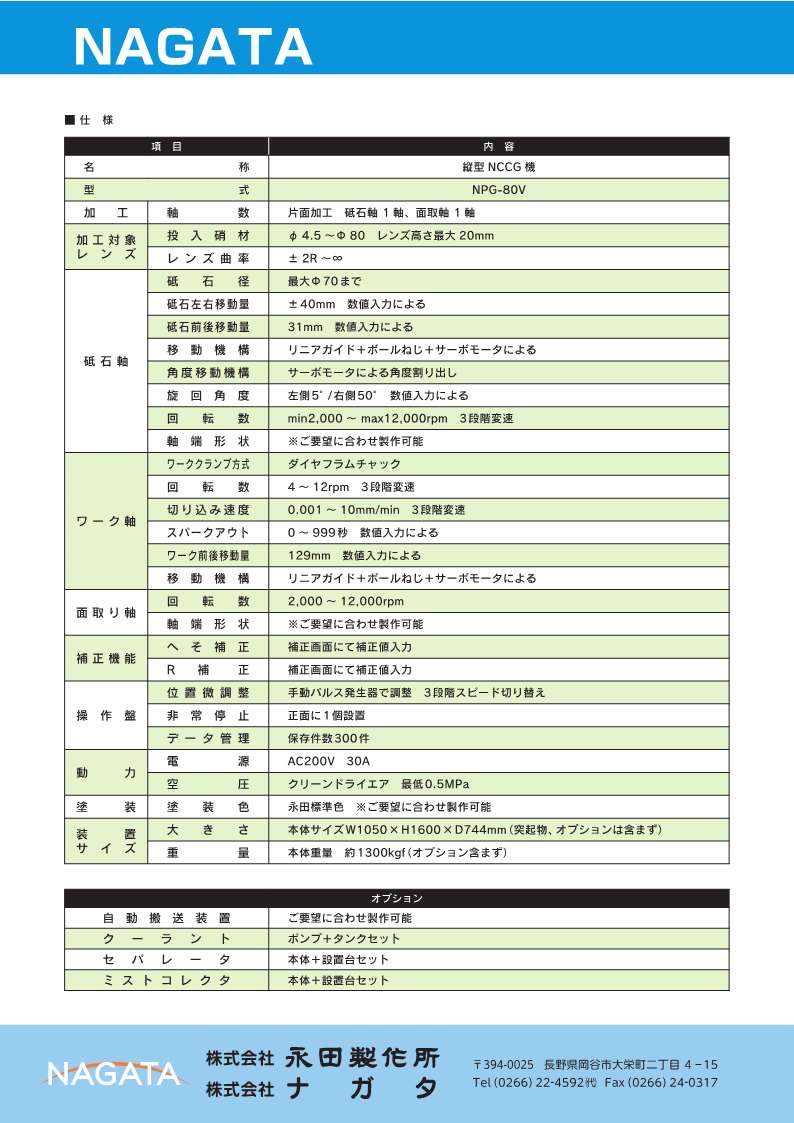
| Lens to be processed | Glass material | φ20~80mm lens height max. 20mm |
| Lens curvature | ±R10mm~∞ | |
| Grindstone shaft | Diameter of Grinding stone | up to max φ70mm |
| Horizontal movment amount | ±40mm by value input | |
| Vertical movement amount | -11 mm from θ-center, +20 mm toward chuck side input value (Movement in lens direction) |
|
| Drive Mechanism | Linear Guide+ball screw+servomotor | |
| Tilting Mechanism | roller drive+Angle indexing by servomotor | |
| Swivel AngleSwivel Angle | left side 5°/right side 50° | |
| No. of rotation | 500~8,000rpm(3-step speed setting available) | |
| Motor | 1 unit | |
| No. of spindle | 1 pc | |
| Shaft end shape | Hydraulic Chuck Grinding Wheel Mount φ30 (Miki pulley ETP-E-25RH) |
|
| Work shaft | Chuck shape | Diaphragm chuck |
| Workpiece clamping method | Resin Jaws | |
| No. of rotation | 20~1,200rpm(3-step speed setting available) | |
| Motor | 1unit | |
| Infeed Speed | 0.001~10mm/min input value(3-step speed setting available) | |
| Spark out | 0~999 sec. input value | |
| Vertical movement amount | Upward -15 mm, Downward -144 mm from θ-center input value (Up to diaphragm end face (excluding jaws)) |
|
| Drive Mechanism | Linear Guide+ball screw+servomotor | |
| Correction function | convexity correction and
Δh correction |
Enter compensation values on the compensation screen Manually measure the workpiece and input the error value |
| Grinding liquid | Supply position | 1 Line+Center Water Supply |
| Tank | Rectangular Tank | |
| safety device | front door | Unlocked after a set time following completion of processing (locked via electromagnetic lock) |
| emergency stop | 1 in control box | |
| Control panel | Touch panel | 10.4 inch. |
| Control panel | Automatic, manual, setting screen, etc. switching display | |
| Fine adjustment | Manual pulse generator adjustment | |
| Data management | 20 pcs can be saved | |
| Running function | Full-stroke movement during initial homing after power-on | |
| Power | Power source | AC200V |
| Air pressure source | Clean dry air 0.5MPa | |
| Dimensions | Approx. W1,050×H1,600×D1,100mm(excl. protrusions and conveyor) | |
| Weight | Approx. 1,300kg |
Click to enlarge.